 Tiếng Việt
Conveyor width: 400 mm.
Inlet height: 6000 mm.
Outlet height: 800 mm.
Conveying speed: 15 m/min.
Load capacity: 769 kg (total weight of products within the machine).
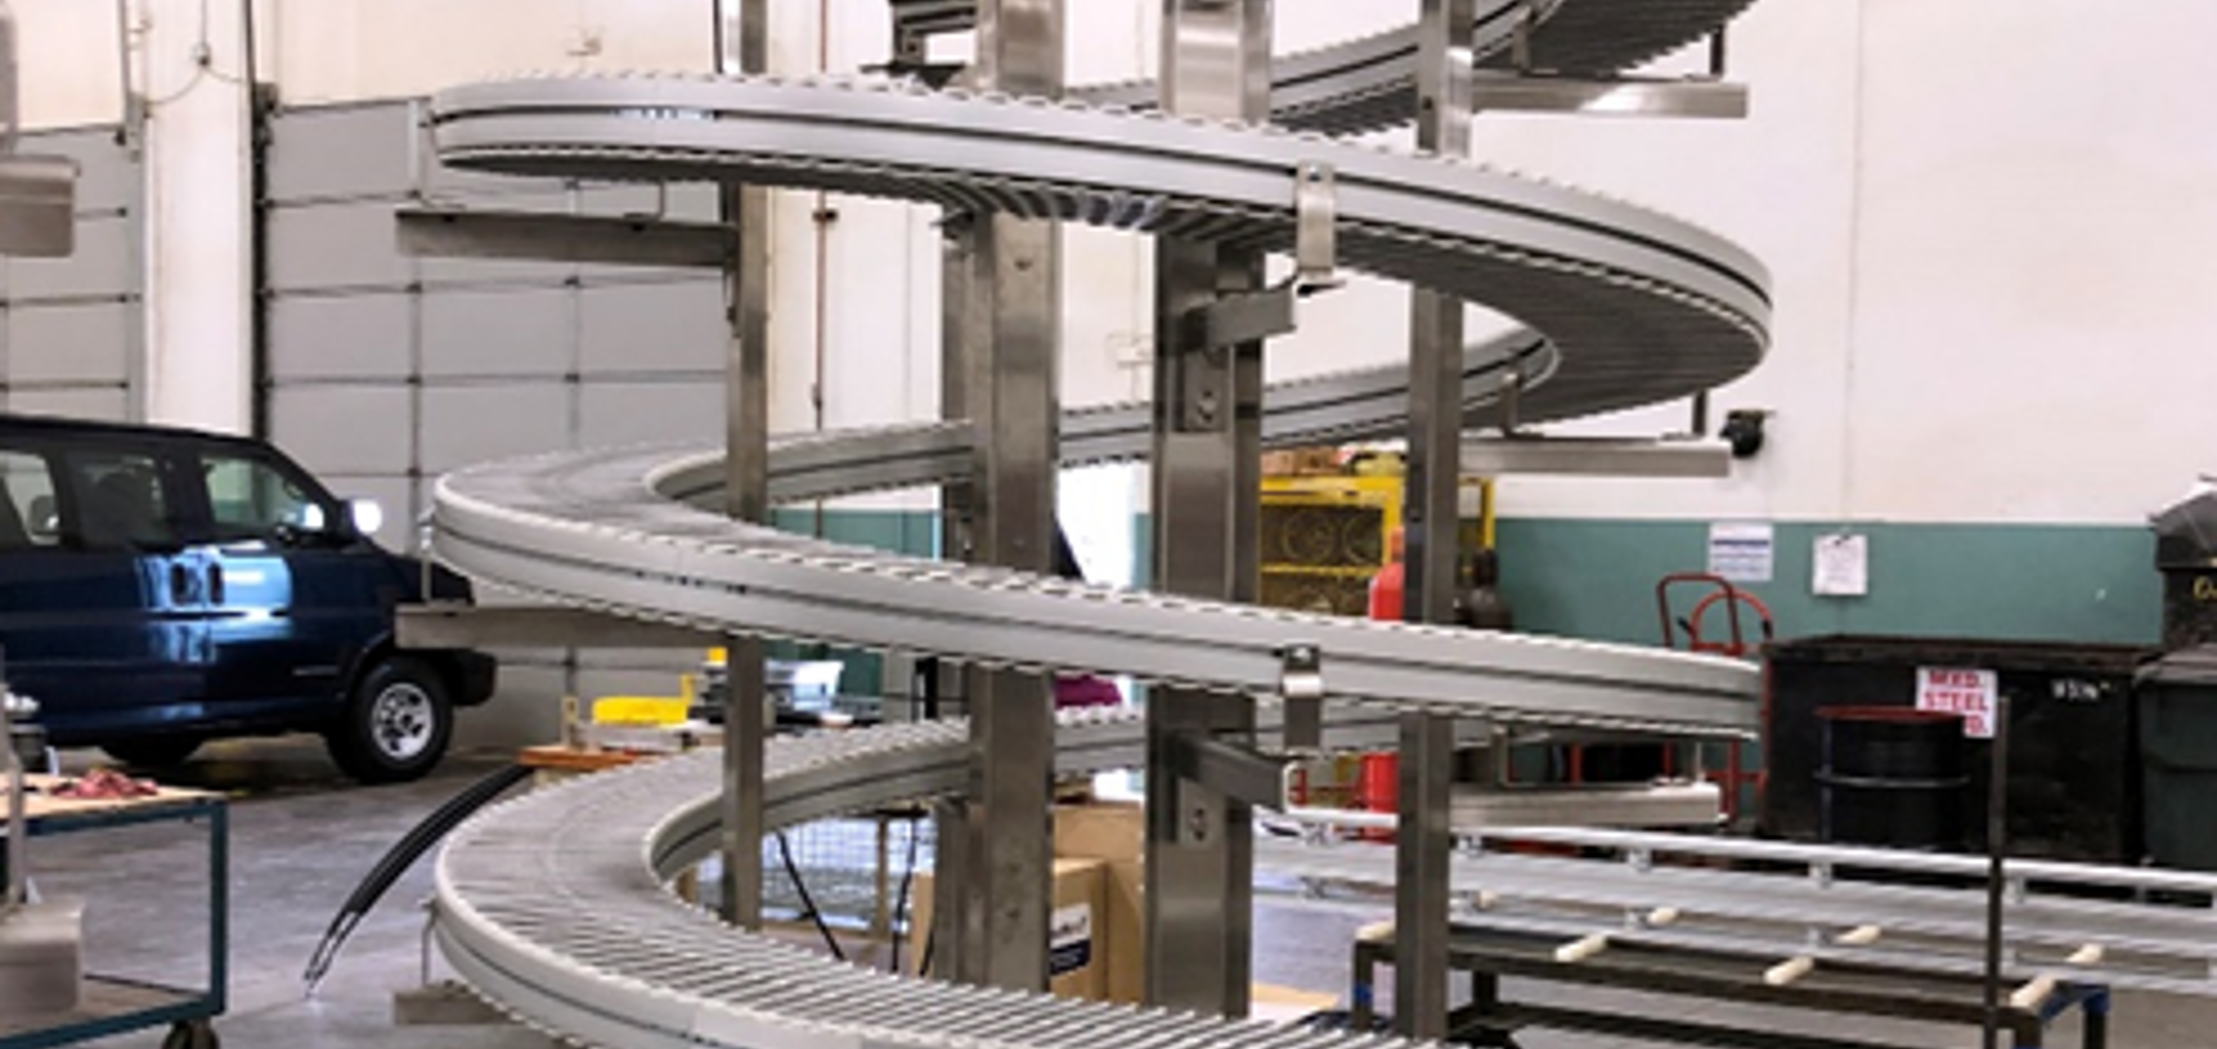
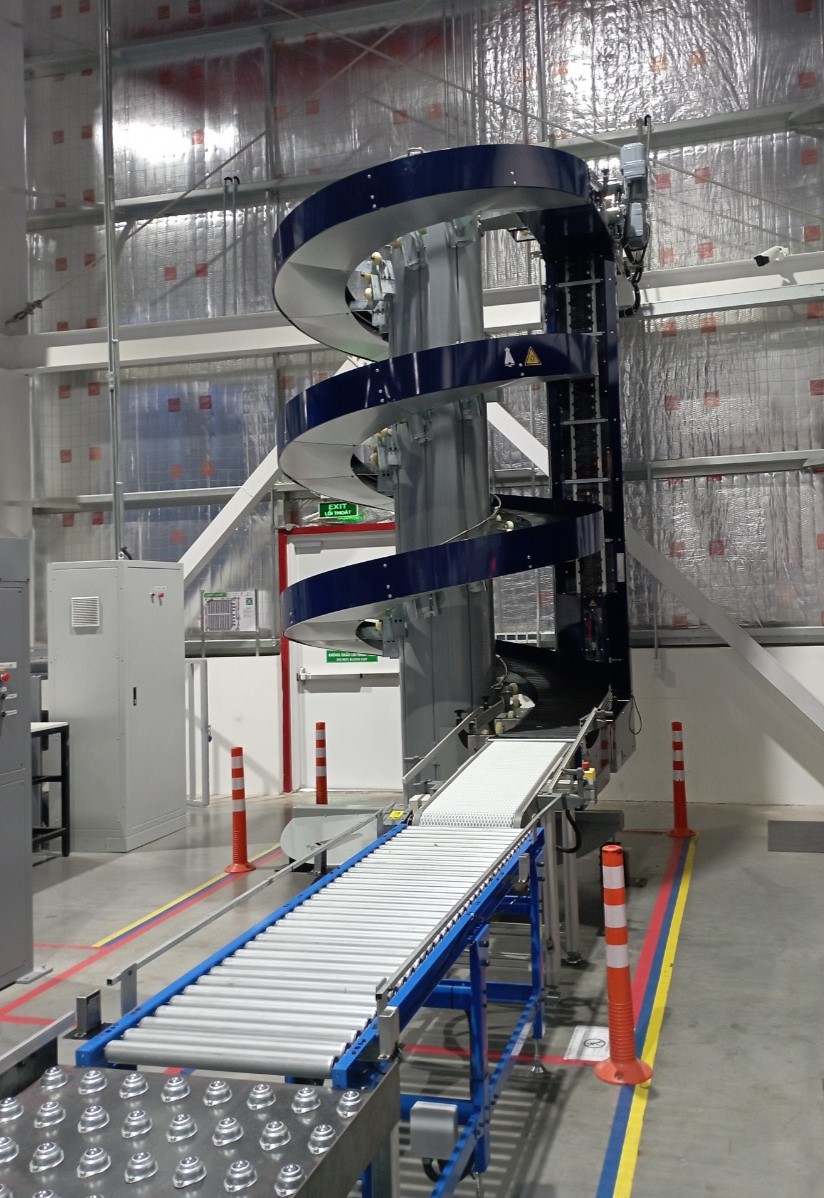
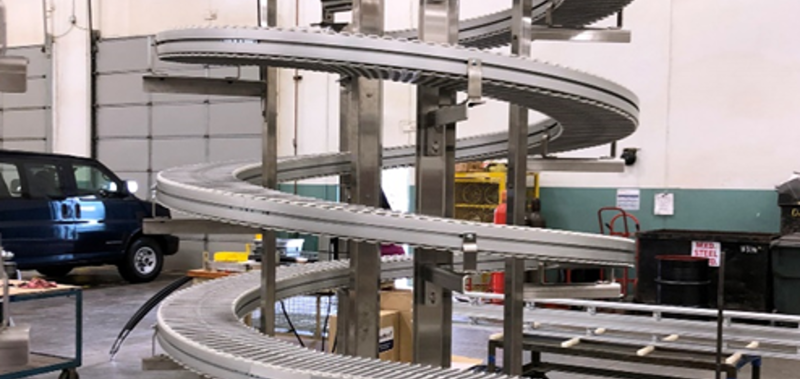
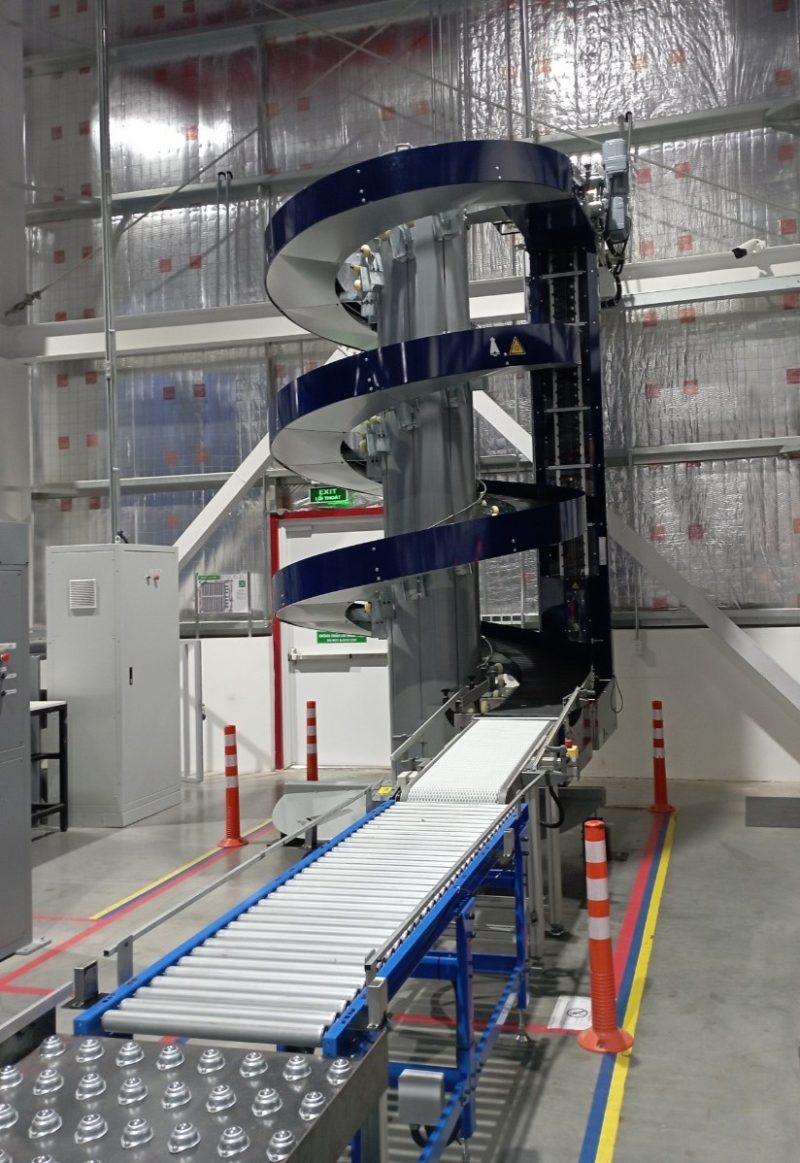
Spiral conveyor
A spiral conveyor is designed to transport products from higher levels to lower levels continuously, safely, and efficiently. It is an optimal solution for factories that need to save floor space while maintaining stable production flow and transport speed.
Related products
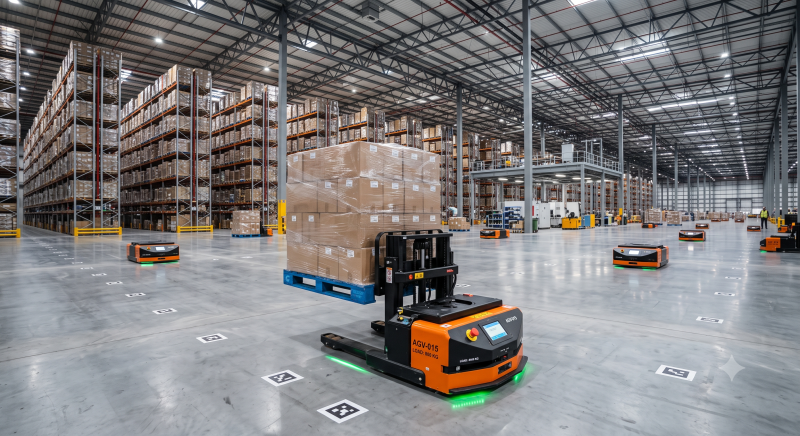
An AGV (Automated Guided Vehicle) robot is an intelligent automated transport solution that optimizes internal logistics within factories. The system enables precise, safe, and continuous movement of raw materials, semi-finished products, or finished goods between production areas. Implementing AGV technology helps businesses reduce manual labor dependency, improve operational flexibility, and enhance the overall automation efficiency of production lines.
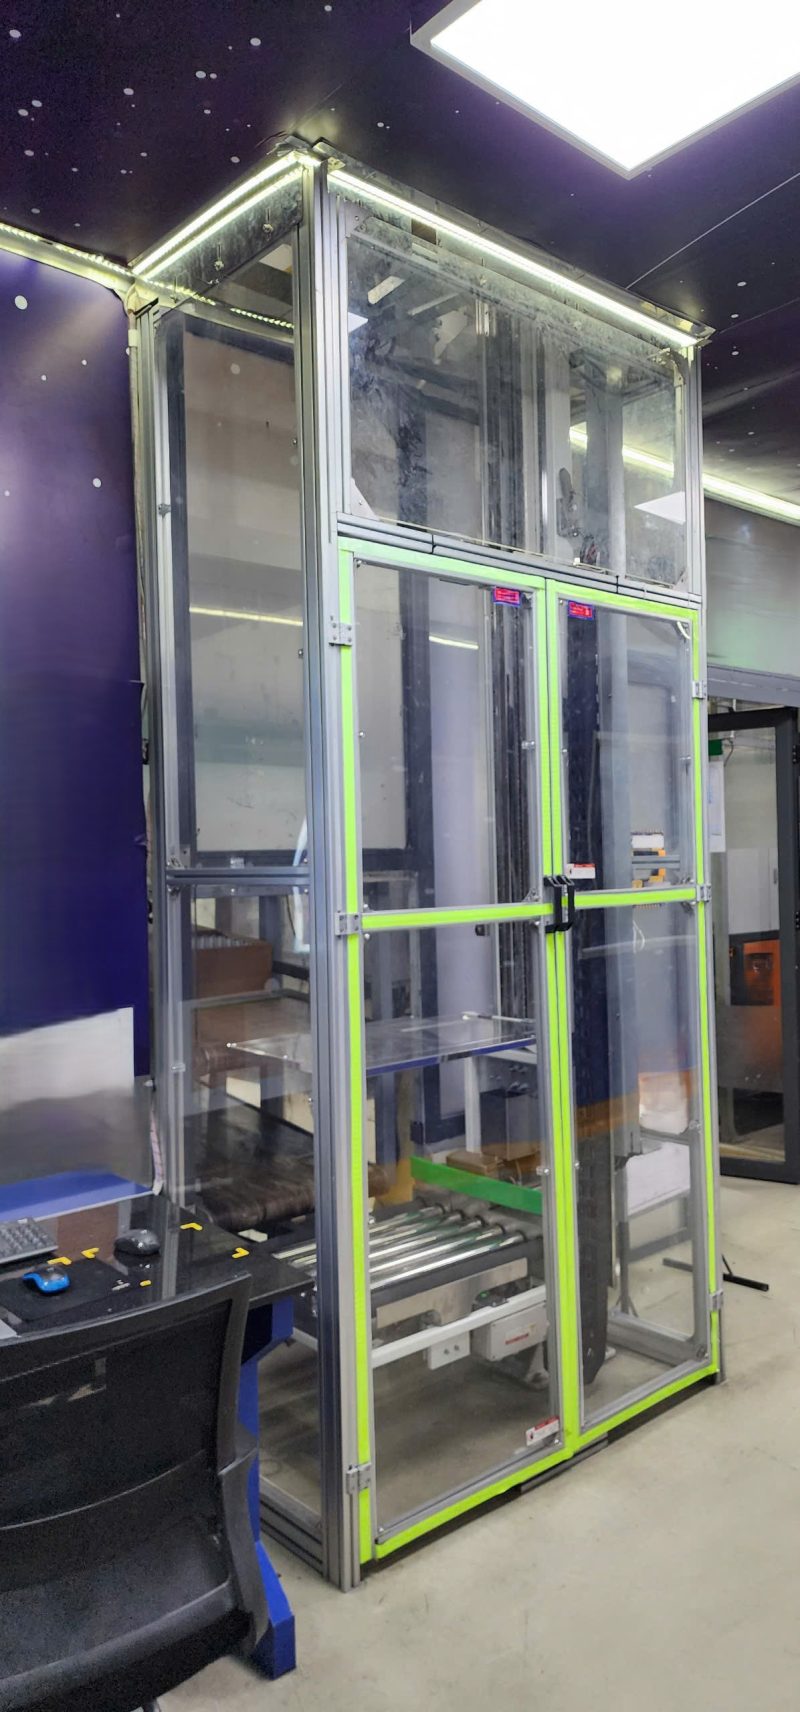
The carton lifter system is designed to optimize the transfer of carton boxes between the cartoner and case packer machines in the packaging line. With a compact, lightweight design and high operational reliability, the system enables precise lifting and lowering of empty cartons while synchronizing with the production line speed. This solution is ideal for factories seeking to automate carton feeding processes, ensuring stable throughput, reducing manual labor, and impro
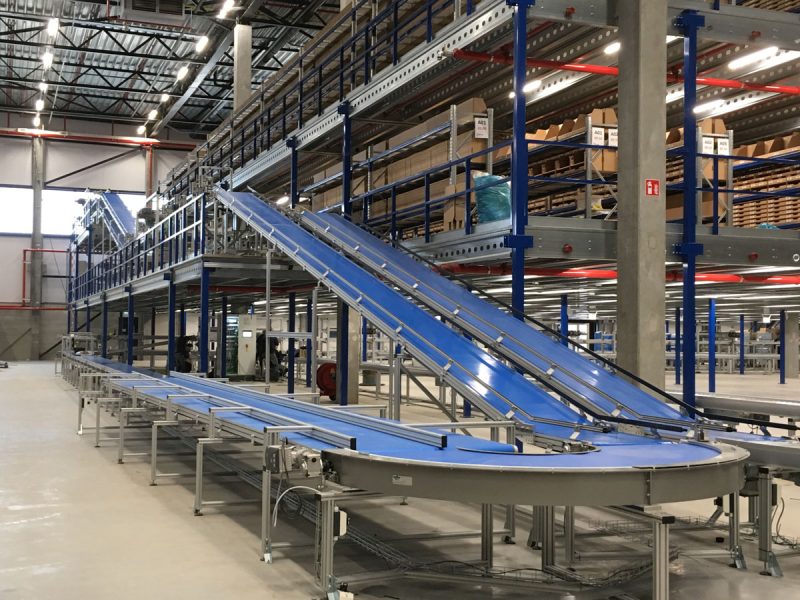
A belt conveyor is a material handling system known for its high durability and heat resistance. With the ability to handle heavy loads, resist impact, and withstand friction, this type of conveyor operates reliably under various environmental conditions, terrains, and transport distances. Belt conveyors are commonly used for handling bulk materials and packaged goods, with two typical configurations: inclined conveyors and horizontal conveyors, providing flexible solutions for different production and logistics needs.
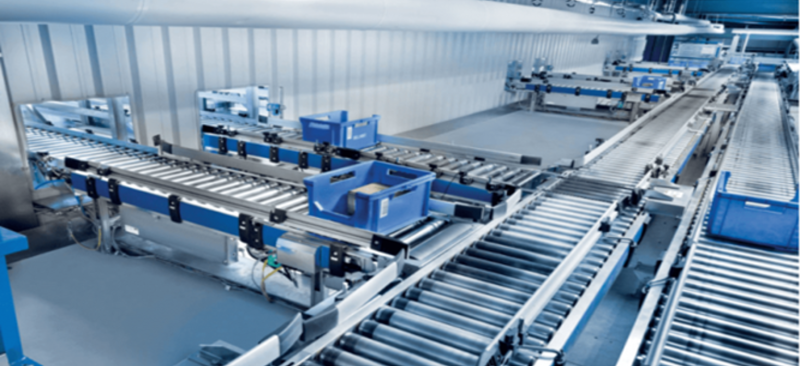
A roller conveyor is a material handling system composed of multiple rollers connected in a sturdy frame, designed to support and move goods efficiently along the production line. The system operates reliably even in dusty or corrosive environments thanks to its high load capacity and durability. Roller conveyors are especially suitable for products with flat and rigid bottoms such as carton boxes, product cases, and trays, helping optimize packaging and internal transportation processes in factories.
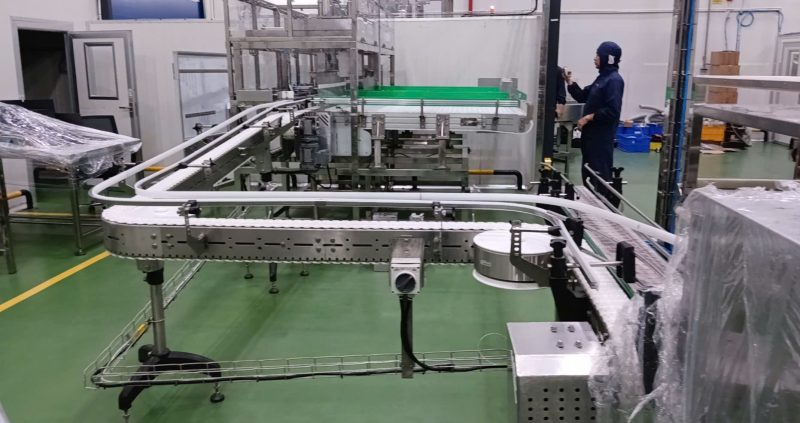
A plastic chain conveyor is an ideal solution for the food processing and manufacturing industries. With the integration of automation systems, it enables safe handling, hygienic operation, and compliance with strict industry standards. Featuring a simple design, high durability, and easy operation, plastic chain conveyors are a preferred choice for businesses seeking to optimize costs while maintaining long-term production efficiency.